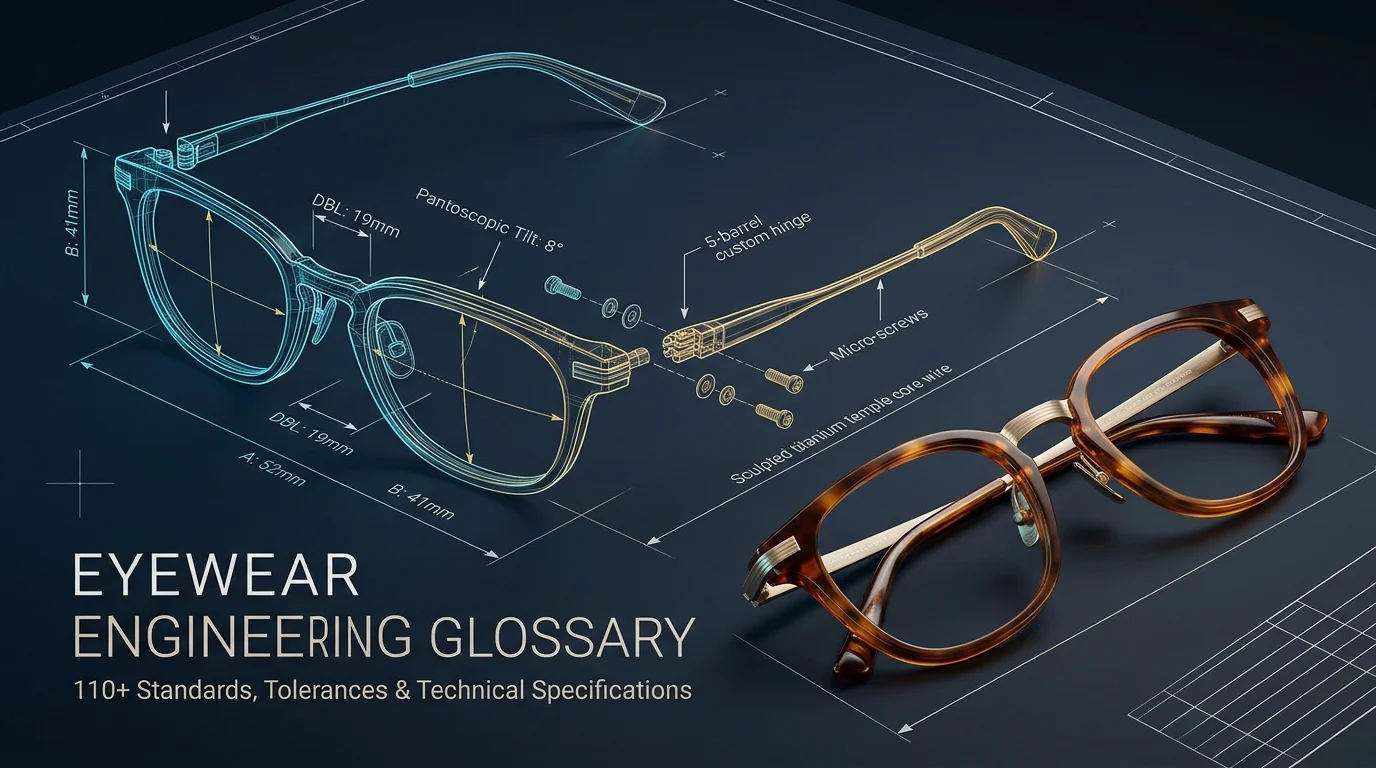
A comprehensive engineering encyclopedia and plain-English reference for eyewear designers, brand founders, and optical buyers. Master 110+ manufacturing specifications—from Mazzucchelli acetate aging and 5-barrel hinge tolerances to pantoscopic tilt, titanium laser welding, and ISO 12870 quality benchmarks.
Welcome to the Eyewear Engineering Glossary & Technical Knowledge Graph, curated by the master toolers and production engineers at Hermitin Optical.
If you are an eyewear brand founder, fashion designer, or procurement manager, you have likely experienced the “lost in translation” gap between creative sketches and factory shop floors. Words like Pantoscopic Tilt, Wire Shooting, Acetate Skiving, or Barrel Tolerance can sound like intimidating aerospace jargon. Yet, understanding these terms is the secret to getting perfect prototypes on the first try, avoiding costly quality disasters, and creating frames that feel like true luxury in your customer’s hands.
This glossary translates 110+ core optical manufacturing terms into clear, plain English, accompanied by exact factory engineering tolerances and practical sourcing advice.
⚡ Quick Jump: 10 Technical Clusters
Click any section below to navigate directly to its engineering terms:
Cluster 1: Frame Anatomy & Sizing Geometry (Terms 1–10)
1. A-Measurement (Lens Width / Eye Size)
- 💡 In Plain English: The horizontal width of a single lens opening at its widest point. It is the first number printed on the inside of a glasses temple (for example, the ‘50’ in 50□20-145).
📐 Technical Definition: The maximum horizontal distance between the vertical bounding lines of the boxed lens aperture, measured in millimeters along the horizontal midline according to the Boxing System (ISO 8624).
- ⚙️ Factory Standards & Tolerances: Factory tolerance is held to ±0.5 mm on finished acetate rims and ±0.25 mm on CNC-milled titanium rims.
- 💼 Sourcing & Brand Takeaway: Directly affects facial proportion and lens thickness. For strong negative prescriptions (-4.00D or higher), keeping the A-measurement under 50 mm prevents thick, unsightly lens edges.
2. B-Measurement (Lens Height / Vertical Depth)
- 💡 In Plain English: The vertical height of the lens opening from the very top to the very bottom.
📐 Technical Definition: The vertical distance between the top and bottom horizontal bounding lines of the boxed lens aperture, measured perpendicular to the horizontal centerline.
- ⚙️ Factory Standards & Tolerances: Standard tolerance is ±0.5 mm for acetate frames and ±0.2 mm for metal eye wires.
- 💼 Sourcing & Brand Takeaway: Critical for progressive (multifocal) lenses. Progressive lenses require a minimum B-measurement of 28 mm to fit distance, intermediate, and reading corridors without cutting off the bottom reading zone.
3. DBL (Distance Between Lenses / Bridge Width)
- 💡 In Plain English: The narrowest space between the two lenses where the frame sits across the nose. It is the middle number printed on the frame arm (the ‘20’ in 50□20-145).
📐 Technical Definition: The shortest horizontal distance separating the nasal eyewires of the left and right rims across the nasal bridge aperture (ISO 8624).
- ⚙️ Factory Standards & Tolerances: Quality control tolerance is strictly held to ±0.3 mm to prevent pupil decentration.
- 💼 Sourcing & Brand Takeaway: Getting DBL wrong causes the glasses to slide down the nose or pinch painfully. Western fit frames typically use 18 mm to 22 mm; Asian / low-bridge fit frames require 16 mm to 18 mm with thicker saddle pads.
4. ED (Effective Diameter)
- 💡 In Plain English: Twice the distance from the center of the lens to its farthest corner. Think of it as the diagonal size of the lens.
📐 Technical Definition: Twice the distance from the geometric center of the lens box to the furthest apex of the lens bevel perimeter, representing the smallest circular lens blank that can yield this shape.
- ⚙️ Factory Standards & Tolerances: Measured via digital CNC frame tracers with ±0.1 mm precision.
- 💼 Sourcing & Brand Takeaway: Essential for cat-eye, pilot aviator, and geometric frames. An exaggerated diagonal point demands larger 75 mm or 80 mm raw lens pucks, increasing lens production costs.
5. Pantoscopic Tilt (Panto Angle)
- 💡 In Plain English: The forward tilt of the front frame toward the wearer’s cheeks. When you look in the mirror, the bottom of the frame should angle slightly toward your cheekbones, not sit straight like a flat windowpane.
📐 Technical Definition: The vertical inclination of the frame front relative to the temples, angling the lower eyewires inward toward the facial plane.
- ⚙️ Factory Standards & Tolerances: Ergonomic standard is 7° to 12° (optimum 8°–10°). Factory inspection tolerance is ±1.5°.
- 💼 Sourcing & Brand Takeaway: Proper pantoscopic tilt aligns the lenses with the natural downward gaze of human eyes, eliminating blurred peripheral vision and headaches.
6. Retroscopic Tilt
- 💡 In Plain English: The opposite of good design: when the bottom of the glasses tilts outwards away from the cheeks, leaning backwards toward the forehead.
📐 Technical Definition: The reverse vertical inclination of the frame front where the bottom of the eyewires tilts away from the cheeks, contrary to human facial anatomy.
- ⚙️ Factory Standards & Tolerances: Regarded as a zero-tolerance assembly defect in factory inspection (< 1° allowable).
- 💼 Sourcing & Brand Takeaway: Causes severe vision distortion and glare bounce on anti-reflective lenses. It is easily corrected during assembly by adjusting the hinge drop angle.
7. Wrap Angle (Face Form / Panoramic Curve)
- 💡 In Plain English: How much the glasses curve around your face. Flat dress frames are almost straight across, while cycling and wrap sunglasses curve snugly around the temples.
📐 Technical Definition: The horizontal dihedral angle at which the left and right frame fronts curve backward around the facial contour relative to the nasal bridge plane.
- ⚙️ Factory Standards & Tolerances: Urban fashion frames carry 0° to 5° wrap; high-performance sports eyewear ranges from 12° to 20° (Base Curve 6 to 8). Tolerance is ±1.0°.
- 💼 Sourcing & Brand Takeaway: Any wrap angle over 5° requires ‘digitally compensated’ prescription lenses. If you put standard prescription lenses in a high-wrap frame, the wearer will feel dizzy and experience fishbowl distortion.
8. Vertex Distance (Back Vertex Distance / BVD)
- 💡 In Plain English: The physical gap between the back of your glasses lens and the front of your eyeball (cornea). Usually about 12 mm to 14 mm.
📐 Technical Definition: The linear millimeter distance between the posterior surface of an optical lens and the anterior apex of the cornea.
- ⚙️ Factory Standards & Tolerances: Anatomical fitting benchmark target is 12 mm to 14 mm.
- 💼 Sourcing & Brand Takeaway: If the vertex distance is too short, eyelashes brush against the lens with every blink. For customers with flatter nose bridges, custom pad arms are required to lift the frame away from the eyelashes.
9. Temple Length
- 💡 In Plain English: The total length of the glasses arm, measured from the hinge screw back to the very tip that rests behind your ear (the ‘145’ in 50□20-145).
📐 Technical Definition: The overall linear length of the frame arm from the central hinge pivot axis to the terminal tip, measured along the curvature contour.
- ⚙️ Factory Standards & Tolerances: Standard industry lengths are 135 mm, 140 mm, 145 mm, and 150 mm, calibrated to ±1.0 mm.
- 💼 Sourcing & Brand Takeaway: The bend should start 10 mm to 15 mm behind the top of the ear. If the temple is too short, it pulls the frame into the nose bridge; if too long, it flaps loosely behind the head.
10. Total Frontal Width (Overall Frame Width)
- 💡 In Plain English: The total end-to-end width of the glasses from the extreme left corner to the extreme right corner.
📐 Technical Definition: The total lateral distance measured from the outermost temporal apex of the left endpiece to the outermost temporal apex of the right endpiece.
- ⚙️ Factory Standards & Tolerances: Tolerance is held to ±1.0 mm across CNC manufacturing batches.
- 💼 Sourcing & Brand Takeaway: The #1 sizing metric online shoppers care about. Narrow faces need <130 mm; Medium is 130–139 mm; Wide is 140–149 mm; Extra-Wide is 150+ mm. Miscalculating this leads to high e-commerce return rates.
Cluster 2: Cellulose Acetate Craft & CNC Milling (Terms 11–22)
11. Cellulose Acetate (CA)
- 💡 In Plain English: The gold standard material for luxury eyewear. Unlike cheap injection-molded petroleum plastic, cellulose acetate is an organic bioplastic made from natural cotton linters and wood pulp. That is why it feels silky, warm to the touch, and can be hand-polished to a glass-like mirror sheen.
📐 Technical Definition: A semi-synthetic organic bioplastic synthesized by acetylating natural cotton linters and wood pulp with acetic anhydride, plasticized with diethyl phthalate (DEP) or eco-plasticizers.
- ⚙️ Factory Standards & Tolerances: Density is 1.28 to 1.32 g/cm³. Raw slabs are calibrated to standard thicknesses: 4.0 mm, 6.0 mm, 8.0 mm, and 10.0 mm (±0.15 mm).
- 💼 Sourcing & Brand Takeaway: Hypoallergenic, flexible, and easily adjusted with heat by opticians. Learn how to select the best grades in our Acetate Material Sourcing Guide.
12. Bio-Acetate (Eco-Friendly / Biodegradable Acetate)
- 💡 In Plain English: Acetate re-engineered for sustainability. The traditional petroleum-based chemical plasticizers are replaced with vegetable-based organic plasticizers, making the frames biodegradable in industrial compost.
📐 Technical Definition: An eco-engineered formulation of cellulose acetate where petroleum-derived plasticizers are replaced with plant-derived alternatives, meeting ISO 14855 and EN 13432 industrial compostability standards.
- ⚙️ Factory Standards & Tolerances: Bio-based carbon content typically exceeds 68% under ASTM D6866 laboratory testing.
- 💼 Sourcing & Brand Takeaway: Essential for European and North American DTC brands targeting eco-conscious consumers. Read our deep dive on Bio-Acetate vs. Standard Cellulose Acetate.
13. Mazzucchelli 1849
- 💡 In Plain English: The ‘Rolls-Royce’ of acetate manufacturers. Based in Castiglione Olona, Italy, Mazzucchelli has been creating the world’s most beautiful, deeply saturated, and crystalline acetate patterns since 1849.
📐 Technical Definition: The preeminent Italian manufacturer of luxury block-cast and extruded cellulose acetate sheets, renowned for proprietary pattern depth, crystallization stability, and chromatic brilliance.
- ⚙️ Factory Standards & Tolerances: Sheet flatness tolerance is < 0.5 mm per meter; shrinkage rate is documented under strict laboratory certificates.
- 💼 Sourcing & Brand Takeaway: Using authentic Mazzucchelli acetate allows brands to charge $250+ retail prices. Buyers instantly recognize the brand name as a hallmark of luxury.
14. Acetate Thermal Curing & Oven Aging (Stabilization)
- 💡 In Plain English: Baking raw acetate in temperature-controlled rooms for days before cutting it. Just like drying fine timber before building furniture, baking flashes off residual solvents so the glasses never warp or lose their shape.
📐 Technical Definition: A factory post-curing process where raw or rough-cut acetate slabs are hung in temperature- and humidity-controlled drying chambers for 72 to 240 hours to flash off residual volatile solvents.
- ⚙️ Factory Standards & Tolerances: Chamber parameters: 45°C to 55°C at 40%–50% relative humidity for 5 to 10 continuous days.
- 💼 Sourcing & Brand Takeaway: Skipping this step is the #1 mistake of cheap factories. Un-aged acetate shrinks and twists after 6 months, causing prescription lenses to pop out unexpectedly.
15. Acetate Skiving (Thickness Shaving)
- 💡 In Plain English: Precision-shaving the thickness of an acetate frame from front to back. It allows you to have a bold, chunky 8 mm vintage look on the front while tapering down to a slim, comfortable 3.5 mm behind the ears.
📐 Technical Definition: A planar shaving process that progressively reduces the gauge of an acetate slab from a heavy front down to a refined taper along the temple shaft or browline.
- ⚙️ Factory Standards & Tolerances: Blade feed tolerance is held to ±0.05 mm.
- 💼 Sourcing & Brand Takeaway: Reduces overall frame weight by up to 35% while preserving a bold, architectural appearance. Solves the complaint that ‘chunky glasses feel too heavy on my nose.’
16. Acetate Block Lamination (Diffusion Bonding)
- 💡 In Plain English: Fusing two or more different sheets of acetate together with heat and pressure to create custom multi-layer effects (for example, black on the outside, crystal neon on the inside).
📐 Technical Definition: The permanent fusion of distinct colored or patterned acetate sheets under hydraulic pressure and solvent/thermal activation to produce bespoke multi-ply laminate blocks.
- ⚙️ Factory Standards & Tolerances: Interface bond strength must withstand > 20 kgf tensile pull without peeling along the seam.
- 💼 Sourcing & Brand Takeaway: Creates signature design looks like tortoiseshell laminated over crystal champagne. Requires precise solvent chemistry to avoid microscopic trapped air bubbles.
17. CNC 5-Axis Profile Routing
- 💡 In Plain English: High-speed computer-guided robotic milling that cuts frame shapes out of solid blocks of acetate with surgical precision.
📐 Technical Definition: Computer Numerical Control (CNC) multi-axis routing using high-speed carbide end mills (18,000 to 24,000 RPM) to cut 2D front contours, bridge facets, and 3D lens retention bevels out of solid acetate slabs.
- ⚙️ Factory Standards & Tolerances: Dimensional cutting tolerance is held to ±0.03 mm.
- 💼 Sourcing & Brand Takeaway: Replaces vintage manual die-punching. Guarantees 100% symmetry between the left and right eyes, making lens assembly effortless.
18. Milling Depth (Lens Groove Cut Depth)
- 💡 In Plain English: The depth of the V-shaped internal groove carved inside the rim where the lens snaps into place.
📐 Technical Definition: The exact vertical penetration depth of the profile cutter creating the V-shaped internal groove inside the eyewire rim that secures the lens bevel.
- ⚙️ Factory Standards & Tolerances: Standard optical bevel depth is 1.2 mm to 1.6 mm (±0.05 mm) with an apex angle of 110° to 120°.
- 💼 Sourcing & Brand Takeaway: If the groove is too shallow (<1.0 mm), lenses pop out when the frame flexes; if cut too deep (>1.8 mm), the rim wall becomes thin and cracks during cold weather.
19. Wire Shooting (Core Wire Infiltration)
- 💡 In Plain English: Shooting a decorative metal wire into the center of the plastic temple arm while the acetate is warm. The wire acts as the arm’s flexible ‘spine’.
📐 Technical Definition: A high-precision thermal process where a stainless steel, titanium, or nickel-silver core wire is driven under pneumo-hydraulic thrust into the heated center of an acetate temple shaft.
- ⚙️ Factory Standards & Tolerances: Acetate is heated to 68°C–72°C; core concentricity is held within ±0.15 mm of centerline.
- 💼 Sourcing & Brand Takeaway: Because raw acetate softens with body heat, the core wire prevents temples from drooping and allows opticians to bend the tips to fit the customer’s ear shape. Custom-engraved wire cores add tremendous perceived value.
20. Hand Scraping (Raspatura Craft)
- 💡 In Plain English: An artisanal hand craft where a master craftsman uses a razor-sharp steel scraper blade to bevel edges and remove robotic CNC tooling ridges by hand.
📐 Technical Definition: A traditional bench finishing craft using a hardened steel scraper to hand-shape frame bevels, eliminate tool ridges, and sculpt organic contours.
- ⚙️ Factory Standards & Tolerances: Removes 0.05 mm to 0.1 mm of surface material per stroke.
- 💼 Sourcing & Brand Takeaway: Gives luxury eyewear an organic, silky softness that automated tumbling alone cannot replicate. Standard practice in high-end Japanese and Italian boutique production lines.
21. Miter Cut (45° Endpiece Joint)
- 💡 In Plain English: Cutting the meeting point between the temple arm and the front frame at a precise 45-degree angle, so they close together with a flush, invisible seam.
📐 Technical Definition: A precision 45-degree angle sliced through both the temporal frame lug and the anterior temple butt, enabling them to meet in a flush, seamless joint when opened.
- ⚙️ Factory Standards & Tolerances: Angular cutting tolerance is ±0.25°; joint seam gap must be < 0.08 mm.
- 💼 Sourcing & Brand Takeaway: The hallmark of luxury construction. Any machining error creates an ugly light gap or prevents the temple from opening to the required 90°–95° angle.
22. Havana / Tortoiseshell Color Blending
- 💡 In Plain English: The classic speckled color pattern featuring warm amber, honey, dark chocolate, and cognac tones blended together to mimic natural sea turtle shells.
📐 Technical Definition: A proprietary pattern classification of cellulose acetate mimicking natural tortoiseshell through irregular mosaic distributions of amber, cognac, dark chocolate, and honey flakes.
- ⚙️ Factory Standards & Tolerances: Color batch consistency is checked under D65 artificial daylight light-boxes against master control swatches.
- 💼 Sourcing & Brand Takeaway: Because the colored chips disperse randomly inside the acetate block, every single finished frame is unique, giving your customers a truly one-of-a-kind piece.
Cluster 3: Tumbling, Polishing & Surface Finishing (Terms 23–32)
23. Tumbling / Barreling (Rotary Tumbling)
- 💡 In Plain English: Putting raw cut frames into large wooden barrels filled with hardwood pegs and polishing creams, tumbling them continuously for 3 to 5 days until they become silky smooth.
📐 Technical Definition: A multi-stage mechanical mass-finishing process where rough-cut acetate components rotate inside octagonal wooden barrels filled with granules and polishing pastes to deburr and polish surfaces.
- ⚙️ Factory Standards & Tolerances: Standard Hermitin cycle: 4 stages lasting 72 to 120 total hours at 28–32 RPM.
- 💼 Sourcing & Brand Takeaway: Replaces aggressive sandpapering. Thorough tumbling rounds every edge comfortably without dulling crisp architectural lines. Read our full guide on The Art of Acetate Eyewear Polishing.
24. Beechwood & Birch Pegs
- 💡 In Plain English: Small geometric hardwood chips cut from European beech, birch, or bamboo. They act as gentle rubbing stones inside tumbling barrels, carrying polishing creams across the frames.
📐 Technical Definition: Hardwood geometric granules (rhomboids, cubes, cylinders) acting as carriers for micro-abrasive polishing pastes during barrel tumbling.
- ⚙️ Factory Standards & Tolerances: Peg moisture content is strictly maintained below 8% to prevent swelling or paste clumping.
- 💼 Sourcing & Brand Takeaway: Dense hardwood provides the exact natural friction needed to polish plant-based acetate without scratching or denting the frame surfaces.
25. Pumice Grinding Compound (Coarse Tumbling)
- 💡 In Plain English: Crushed volcanic rock powder mixed with mineral oils, used in the first 24–36 hours of tumbling to erase sharp CNC cutter grooves.
📐 Technical Definition: Pulverized volcanic pumice stone (120 to 240 mesh) lubricated with mineral oil, used in the first stage of tumbling to eliminate machining marks.
- ⚙️ Factory Standards & Tolerances: Reduces surface roughness (Ra) from ~3.2 µm down to ~0.8 µm over 24 to 36 hours.
- 💼 Sourcing & Brand Takeaway: Must be thoroughly washed off before stage two. If any coarse pumice grain contaminates the fine polish barrels, it will ruin the final mirror gloss.
26. Tripoli Buffing Compound
- 💡 In Plain English: A fine grey-brown polishing paste used in intermediate dry tumbling and rotary buffing wheels to remove micro-scratches.
📐 Technical Definition: A microcrystalline silica-based polishing paste used in intermediate tumbling and high-speed rotary cloth mop polishing.
- ⚙️ Factory Standards & Tolerances: Applied to rotary wheels spinning at 1,400 to 1,800 RPM with light contact pressure.
- 💼 Sourcing & Brand Takeaway: Bridges the gap between rough smoothing and deep shine. Over-buffing with tripoli can soften sharp step-down bevels.
27. Rouge Luster Wheel (Final Cotton Buffing)
- 💡 In Plain English: The final polishing stage using ultra-fine jeweler’s rouge wax applied to soft, spinning cotton flannel wheels to bring out a brilliant mirror shine.
📐 Technical Definition: The final dry polishing operation using ultra-fine aluminum oxide or iron oxide rouge applied to ventilated soft flannel or bleached cotton rotary wheels.
- ⚙️ Factory Standards & Tolerances: Wheel speed: 1,200 RPM; achieves deep specular mirror gloss with surface roughness Ra < 0.05 µm.
- 💼 Sourcing & Brand Takeaway: Creates the deep ‘wet-look’ gloss that customers fall in love with when they open luxury eyewear packaging.
28. Mirror Polishing (Speculare Finishing)
- 💡 In Plain English: The pinnacle of frame polishing: surfaces so smooth and glossy that reflections look like a crystal-clear mirror with zero haze or swirl marks.
📐 Technical Definition: The highest level of optical surface finishing on acetate or metal frames, characterized by flawless reflection clarity without microscopic waves or hazing.
- ⚙️ Factory Standards & Tolerances: Inspected under 1,000-lux halogen lamps with zero visible micro-hazing at 30 cm viewing distance.
- 💼 Sourcing & Brand Takeaway: Directly affects the luxury feel and longevity of the glasses. Highly polished acetate resists sweat and skin acid absorption far better than unpolished plastic.
29. Orange Peel Defect
- 💡 In Plain English: An ugly, dimpled surface defect that looks like the skin of an orange, caused when an inexperienced polisher presses too hard against a hot polishing wheel.
📐 Technical Definition: A surface blemish characterized by an irregular, dimpled texture caused by localized heat buildup during aggressive rotary buffing.
- ⚙️ Factory Standards & Tolerances: Classed as a critical visual rejection defect under ISO 12870 inspection standards.
- 💼 Sourcing & Brand Takeaway: Occurs when friction heat partially melts the surface plasticizer. The frame must be cooled down, hand-scraped, and completely re-tumbled from scratch.
30. Ultrasonic Degreasing
- 💡 In Plain English: Dipping frames into a warm cleaning bath that vibrates with high-frequency sound waves, instantly blasting away dried polishing wax from hinge pockets and screw threads.
📐 Technical Definition: An automated cleaning stage using high-frequency sound waves (28 kHz to 40 kHz) in warm aqueous detergent baths to dislodge residual polishing pastes.
- ⚙️ Factory Standards & Tolerances: Bath temperature is maintained at 40°C to 45°C for 180 to 300 seconds.
- 💼 Sourcing & Brand Takeaway: Ensures no sticky white polishing residue remains hidden inside hinge barrels or lens grooves when the customer receives their glasses.
31. Edge Chamfering (Micro-Beveling)
- 💡 In Plain English: Gently rounding off the razor-sharp 90-degree outside edges of the frame front and arms by about 0.3 mm.
📐 Technical Definition: The deliberate application of a minute 45-degree angle (0.2 mm to 0.5 mm) along the exterior edges of acetate fronts and temple stems.
- ⚙️ Factory Standards & Tolerances: Held to ±0.05 mm via 5-axis CNC chamfer cutter paths.
- 💼 Sourcing & Brand Takeaway: Eliminates ‘knife-edge’ sharpness that irritates the skin behind the ears and prevents frame edges from chipping if accidentally dropped.
32. Acetone Vapor Polishing (Cautionary Term)
- 💡 In Plain English: A cheap factory shortcut where plastic is held over boiling acetone steam to melt the surface into an instant shine in 10 seconds, instead of 4 days of wooden tumbling.
📐 Technical Definition: A rapid finishing method where acetate is exposed to heated acetone vapors, melting the exterior surface into an instant gloss without mechanical buffing.
- ⚙️ Factory Standards & Tolerances: Strictly prohibited in tier-1 luxury manufacturing.
- 💼 Sourcing & Brand Takeaway: While it saves money, vapor polishing strips away plasticizers, leaving frames brittle and prone to cracking within 6 to 12 months. Hermitin exclusively uses 100% mechanical barreling and hand-buffing.
Cluster 4: Metal & Titanium Metallurgy & Tooling (Terms 33–42)
33. Pure Titanium (JIS Grade 2 Alpha Titanium)
- 💡 In Plain English: Pure, unalloyed titanium. It is featherlight, 100% rust-proof, and completely hypoallergenic (it will never cause skin rashes or turn green).
📐 Technical Definition: An unalloyed alpha-phase titanium metal possessing minimum 99.2% purity, offering ultra-lightweight density (4.51 g/cm³), complete biocompatibility, and immune resistance to corrosion.
- ⚙️ Factory Standards & Tolerances: Tensile strength: 345 to 510 MPa; Vickers hardness: HV 160–200.
- 💼 Sourcing & Brand Takeaway: The gold standard for luxury metal frames. 48% lighter than traditional brass/nickel silver frames. Requires specialized argon-gas vacuum chambers for laser welding.
34. Beta-Titanium (Spring Titanium / Ti-15V-3Cr-3Sn-3Al)
- 💡 In Plain English: A super-flexible titanium alloy that acts like a spring. You can bend it into a circle and it snaps right back into its original shape without bending or breaking.
📐 Technical Definition: A metastable titanium alloy compounded with vanadium, chromium, tin, and aluminum, delivering extraordinary elasticity, spring-back recovery, and high tensile endurance.
- ⚙️ Factory Standards & Tolerances: Tensile strength exceeds 980 to 1,150 MPa; elasticity modulus: ~80 GPa (twice the flexibility of pure titanium).
- 💼 Sourcing & Brand Takeaway: Perfect for flexible bridge arches, rimless temples, and lightweight sunglasses that adjust to any head width without pinching. Read our Pure vs. Beta-Titanium Guide.
35. Memory Metal (Nitinol)
- 💡 In Plain English: A ‘smart’ metal alloy made of nickel and titanium that remembers its shape. You can literally twist the bridge 360 degrees or tie the temple in a knot, and it bounces straight back.
📐 Technical Definition: An equiatomic nickel-titanium smart alloy exhibiting superelasticity, allowing frames to endure extreme deformations while instantly rebounding to their exact original geometry.
- ⚙️ Factory Standards & Tolerances: Operates across an active shape-recovery window of -10°C to +40°C.
- 💼 Sourcing & Brand Takeaway: Huge selling point for children’s glasses, active sports eyewear, and unbreakable everyday readers. Requires mechanical crimping because it cannot be soldered with standard silver paste.
36. Stainless Steel (AISI 304 & Medical 316L)
- 💡 In Plain English: Surgical-grade steel that allows frames to be laser-cut into ultra-thin, sleek sheets (under 0.8 mm thick). It is strong, springy, and affordable.
📐 Technical Definition: A chromium-nickel iron alloy (18% Cr, 10% Ni in 304; 2%–3% Mo added in 316L) celebrated for high tensile rigidity, ultra-thin sheet workability, and sweat corrosion resistance.
- ⚙️ Factory Standards & Tolerances: Sheet stock rolled to ultra-thin profiles: 0.5 mm to 0.8 mm (±0.02 mm).
- 💼 Sourcing & Brand Takeaway: Enables modern minimalist flat-sheet screwless designs (like Mykita or ic! berlin styles). Highly sweat-resistant when specified in medical grade 316L. Learn more in our Titanium vs. Stainless Steel Comparison.
37. Monel Alloy
- 💡 In Plain English: A traditional copper-nickel alloy that has been the workhorse material for commercial metal eyeglasses for decades.
📐 Technical Definition: A copper-nickel base metal alloy (approx. 63%–67% nickel, 28%–34% copper, plus iron and manganese) traditionally used as the core workhorse material for commercial metal eyewear.
- ⚙️ Factory Standards & Tolerances: Tensile strength: 480 to 620 MPa.
- 💼 Sourcing & Brand Takeaway: Easy to shape and solder, but contains nickel. For European sales, Monel frames must receive a thick protective plating and polyurethane clear coat to pass strict EU nickel-allergy laws.
38. Nickel Silver (German Silver / Maillechort)
- 💡 In Plain English: A stiff, easy-to-solder metal alloy containing copper, zinc, and nickel (despite its name, it contains zero real silver).
📐 Technical Definition: A copper-zinc-nickel alloy (typically 60% Cu, 20% Ni, 20% Zn) prized for mechanical rigidity, crisp stamping definition, and easy brazing.
- ⚙️ Factory Standards & Tolerances: Commonly used for bridge blanks, endpiece lugs, and temple core wires.
- 💼 Sourcing & Brand Takeaway: Stiff and holds crisp stamped patterns very well. Always finished with electroplating or clear lacquers to prevent direct skin contact.
39. Eye Wire Profiling & Rimlock Drawing
- 💡 In Plain English: Drawing solid metal wire through shaped diamond dies to create the grooved metal ring that wraps around and locks the lens into place.
📐 Technical Definition: The continuous mechanical drawing of solid metal wire through shaped diamond dies to form a grooved cross-section profile designed to lock and cradle the lens bevel.
- ⚙️ Factory Standards & Tolerances: Profile internal groove dimensions held to ±0.02 mm.
- 💼 Sourcing & Brand Takeaway: Ensures the metal eyewire closes tightly around the lens without leaving an ugly gap where the tiny rimlock screw tightens.
40. High-Frequency Induction Brazing (Silver Soldering)
- 💡 In Plain English: Joining metal frame pieces together using localized electromagnetic heat and silver alloy solder.
📐 Technical Definition: The automated joining of metal eyewear components (bridge to eyewire, pad arm to rim) using localized electromagnetic induction heating and silver-based flux solder pastes.
- ⚙️ Factory Standards & Tolerances: Operating temperature: 620°C to 680°C; joint shear resistance must exceed > 250 N.
- 💼 Sourcing & Brand Takeaway: Focuses heat on a tiny 2 mm point, preventing the rest of the frame from softening and losing its springiness.
41. Laser Micro-Welding (Nd:YAG Pulse Laser)
- 💡 In Plain English: Using high-tech laser pulses to weld titanium pieces together inside an argon-gas chamber with microscopic precision, without any messy solder paste.
📐 Technical Definition: An optical welding technology delivering concentrated millisecond laser energy bursts inside an argon inert gas chamber to join titanium and stainless steel parts without flux solder.
- ⚙️ Factory Standards & Tolerances: Weld spot diameter calibrated to 0.2 mm to 0.6 mm with zero oxidation discoloration.
- 💼 Sourcing & Brand Takeaway: The only way to weld pure titanium. Produces welds that are virtually invisible and as strong as the original metal itself.
42. IP Vacuum Plating (Ion Plating / PVD)
- 💡 In Plain English: Plating metal frames inside an aerospace vacuum plasma chamber. Vaporized titanium and gold atoms are bonded molecularly to the frame surface, creating a finish that will never chip, flake, or tarnish.
📐 Technical Definition: Physical Vapor Deposition (PVD) carried out in high-vacuum plasma chambers where titanium, zirconium, or chromium atoms are vaporized and deposited as an ultra-hard ceramic film.
- ⚙️ Factory Standards & Tolerances: Coating thickness: 0.5 µm to 2.5 µm; surface hardness up to HV 1,800–2,500; salt spray resistance > 96 hours.
- 💼 Sourcing & Brand Takeaway: 5 to 10 times more durable than old-fashioned wet electroplating. Essential for luxury gold, gunmetal, and matte black sunglasses that must resist sea salt and acidic human sweat.
Cluster 5: Hinges, Screws & Hardware Articulation (Terms 43–52)
43. Barrel Hinge (Knuckle Joint)
- 💡 In Plain English: The mechanical metal hinge that connects the front of the frame to the temple arms. The ‘barrels’ are the small metal rings that interlock like knuckles on a hand, held together by a screw.
📐 Technical Definition: A mechanical hinge consisting of alternating cylindrical metal knuckles (barrels) interleaved and locked together by a vertical threaded hinge screw or pin.
- ⚙️ Factory Standards & Tolerances: Knuckle bore hole alignment tolerance is held to ±0.015 mm.
- 💼 Sourcing & Brand Takeaway: The foundation of optical engineering. Learn more in our guide on Why Eyewear Hinges Matter for Durability and Retail Value.
44. 3-Barrel Hinge
- 💡 In Plain English: A lightweight hinge with 3 interlocking rings (two on one side, one on the other).
📐 Technical Definition: A barrel hinge configuration featuring two interlocking knuckles on the frame endpiece and one central knuckle on the temple arm, secured with a single screw.
- ⚙️ Factory Standards & Tolerances: Lateral play tolerance: < 0.1 mm; torque resistance: 0.8 to 1.2 kgf·cm.
- 💼 Sourcing & Brand Takeaway: Slim and compact. Perfect for thin acetate frames, delicate optical spectacles, and wire metal sunglasses.
45. 5-Barrel Hinge
- 💡 In Plain English: The industry benchmark for premium acetate sunglasses. It has 5 interlocking rings (three on one side, two on the other), making it sturdy and solid.
📐 Technical Definition: An articulation system comprising three knuckles on the front lug intermeshing with two knuckles on the temple, offering superior resistance against lateral twist.
- ⚙️ Factory Standards & Tolerances: Factory torque preset: 1.2 to 1.6 kgf·cm; rated for minimum 15,000 cycle openings.
- 💼 Sourcing & Brand Takeaway: Provides that smooth, satisfying, heavy-glide feeling when the customer opens and closes the sunglasses. Will not wobble or loosen over time.
46. 7-Barrel Hinge
- 💡 In Plain English: The tank of eyewear hinges: 7 heavy-duty interlocking rings (four on one side, three on the other). Built for bold, chunky architectural frames.
📐 Technical Definition: A heavy-duty vintage-inspired hinge assembly utilizing four knuckles on the frame lug and three on the temple, creating an ultra-robust 7-plane interlocking shear junction.
- ⚙️ Factory Standards & Tolerances: Hinge plate width: 5.0 mm to 7.0 mm; withstands > 25 kgf lateral twisting force.
- 💼 Sourcing & Brand Takeaway: The hallmark of luxury 8 mm and 10 mm Japanese and European collector frames. Provides indestructible mechanical durability.
47. Spring Hinge (Flex Hinge)
- 💡 In Plain English: A hinge with a hidden spring inside that allows the temple arms to bend outward past 90 degrees without snapping, then spring back gently against the head.
📐 Technical Definition: An internal mechanical hinge cartridge housing a tempered steel spring and plunger that allows temples to flex outward 10° to 15° beyond the standard 90° opening angle.
- ⚙️ Factory Standards & Tolerances: Elastic spring stroke: 2.0 mm to 3.5 mm; fatigue endurance tested to > 30,000 continuous cycles.
- 💼 Sourcing & Brand Takeaway: Prevents the glasses from squeezing the sides of wide heads and keeps them from slipping during daily movement. Popular for reading glasses and executive optical frames.
48. OBE Hinge Systems
- 💡 In Plain English: The premier German brand of optical hinges and screws. When an optical buyer hears ‘OBE hinges’, they know the hardware is top-tier German engineering.
📐 Technical Definition: Precision optical articulation hardware engineered and manufactured by OBE GmbH in Germany, globally renowned for zero-tolerance alloy machining and self-locking screw technologies.
- ⚙️ Factory Standards & Tolerances: Pinhole roundness tolerance held to ±0.005 mm; screw failure rate < 1 in 100,000 units.
- 💼 Sourcing & Brand Takeaway: Specifying authentic German OBE hinges immediately elevates your brand above generic fashion sunglasses in the eyes of optical stores and distributors.
49. Comotec Spring Hinge
- 💡 In Plain English: High-performance spring hinges engineered by Comotec (France), famous for sealed spring barrels that never squeak, leak oil, or lose their spring tension.
📐 Technical Definition: High-performance modular spring hinge mechanisms designed by Comotec (France), famous for sealed spring barrels, smooth kinetic damping, and fatigue longevity.
- ⚙️ Factory Standards & Tolerances: Certified under stringent European optical testing standards for > 40,000 cycle flexures.
- 💼 Sourcing & Brand Takeaway: Highly favored by sports-lifestyle and executive prescription brands requiring ultra-reliable, long-lasting temple flex mechanisms.
50. Rivet Hinge Insertion (Through-Pin Staking)
- 💡 In Plain English: Fastening the hinges with two solid metal pins driven straight through the acetate and hammered flat on the outside. Those two small metal dots you see on the front of vintage Ray-Bans or Moscot frames? Those are functional rivets.
📐 Technical Definition: The traditional assembly method where front and temple hinge plates are anchored using twin solid metal pins (rivets) driven entirely through the acetate and peened flat on the exterior surface.
- ⚙️ Factory Standards & Tolerances: Rivet head flushness tolerance: +0.05 / -0.00 mm; zero internal acetate crazing.
- 💼 Sourcing & Brand Takeaway: Far stronger than heat-glued hinges. Dual functional rivets serve as authentic luxury design details that vintage eyewear aficionados look for.
51. Ultrasonic Heat Staking (Hot Embedding)
- 💡 In Plain English: Melting the base of the hinge directly into the acetate using ultrasonic vibrations, leaving the outside of the frame completely clean with no visible rivets.
📐 Technical Definition: An automated manufacturing technique where high-frequency ultrasonic vibrations or thermal induction heat an anchor-footed hinge plate, allowing it to sink into raw acetate.
- ⚙️ Factory Standards & Tolerances: Insertion depth precision held to ±0.08 mm with zero exterior bubble eruption.
- 💼 Sourcing & Brand Takeaway: Provides a super-clean, modern exterior look with zero visible hardware. Requires strict factory temperature control to avoid bubbling the plastic.
52. Nylok / Teflon-Coated Hinge Screw
- 💡 In Plain English: A hinge screw coated with a tiny drop of blue nylon resin that locks the threads tight so the screw never backs out and falls out on the customer.
📐 Technical Definition: A micro-threaded stainless steel hinge screw featuring an engineered blue nylon or PTFE patch bonded onto the threads, acting as a permanent vibration-resistant lock.
- ⚙️ Factory Standards & Tolerances: Thread pitch: M1.0 to M1.4; preserves friction torque over 500+ repeat openings.
- 💼 Sourcing & Brand Takeaway: Eliminates the #1 customer warranty return in the eyewear industry: loose arms and lost hinge screws. Standard on all Hermitin production runs.
Cluster 6: Injection Molding & Synthetic Polymers (Terms 53–60)
53. TR90 (Grilamid Swiss EMS)
- 💡 In Plain English: A miracle memory plastic invented in Switzerland. It is featherlight, virtually unbreakable, and can be twisted like a pretzel without snapping.
📐 Technical Definition: A transparent copolyamide (nylon) thermoplastic synthesized by EMS-Grivory in Switzerland, famed for low density (1.14 g/cm³), memory elasticity, and extreme impact resistance.
- ⚙️ Factory Standards & Tolerances: Melt processing temperature: 260°C to 280°C; mold temperature: 70°C to 90°C.
- 💼 Sourcing & Brand Takeaway: The king of sports sunglasses, kids’ frames, and flexible everyday glasses. Learn how we engineer it in our Sports Eyewear Design & TR90 Manufacturing Guide.
54. Ultem (PEI / Polyetherimide)
- 💡 In Plain English: An aerospace-grade amber resin invented for jet engines. It is heat-proof, featherlight, and strong enough to be molded into ultra-thin, flexible 1.2 mm frames.
📐 Technical Definition: An aerospace-grade amber amorphous thermoplastic engineered by SABIC, featuring exceptional heat resistance (Tg 217°C), rigid tensile strength (105 MPa), and featherlight weight.
- ⚙️ Factory Standards & Tolerances: Allows injection of ultra-thin frame rims down to 1.2 mm cross-section without structural warping.
- 💼 Sourcing & Brand Takeaway: 50% lighter than acetate and completely resistant to sweat, cosmetics, and rubbing alcohol. Huge favorite for lightweight prescription reading frames.
55. Optical Polycarbonate (PC)
- 💡 In Plain English: The bulletproof plastic used in police riot shields and astronaut helmet visors. Virtually impossible to shatter.
📐 Technical Definition: An engineering polymer known for virtually unbreakable impact strength, high refractive index (1.586), and natural 100% UV400 absorption.
- ⚙️ Factory Standards & Tolerances: Impact resistance exceeds FDA 21 CFR 801.410 drop-ball energy by > 400%.
- 💼 Sourcing & Brand Takeaway: Mandatory for ANSI Z87.1 industrial safety glasses, military tactical goggles, and children’s sports protection.
56. Cold Runner vs. Hot Runner Injection Molds
- 💡 In Plain English: In injection molding, cold runners leave behind plastic sprues that must be cut off and thrown away. Hot runners inject liquid plastic directly into the frame cavity with zero waste and zero ugly cut marks.
📐 Technical Definition: Cold runners solidify with every cycle creating sprue waste, whereas hot runners keep plastic continuously molten inside heated manifolds, injecting directly into cavity gates.
- ⚙️ Factory Standards & Tolerances: Hot runner temperature PID-controlled to ±1.0°C across all nozzle drops.
- 💼 Sourcing & Brand Takeaway: Hot runner molds cost 25% more upfront, but they save thousands in plastic resin and eliminate ugly cut scars on finished sunglasses.
57. Weld Line (Knit Line Molding Flaw)
- 💡 In Plain English: An ugly structural defect where two streams of molten plastic meet in the middle (usually at the bridge) and fail to fuse cleanly, leaving a weak seam that snaps easily.
📐 Technical Definition: A visible seam defect formed inside an injection-molded frame where two separate flow fronts of molten polymer converge around a core pin.
- ⚙️ Factory Standards & Tolerances: Zero visible weld lines permitted under 500-lux visual inspection; weld line tensile retention must exceed 85%.
- 💼 Sourcing & Brand Takeaway: A critical failure point. If your factory runs the steel mold too cold, the frame will snap in half at the nose bridge the first time a customer tries to insert a lens.
58. Gate Vestige (Sprue Scar)
- 💡 In Plain English: The tiny rough nub left behind where liquid plastic was pumped into the frame mold and snipped off.
📐 Technical Definition: The minute residual stub of excess plastic left behind on the frame rim where the injection runner was trimmed from the molded component.
- ⚙️ Factory Standards & Tolerances: Must be machined or hand-trimmed flush to < 0.05 mm above base surface.
- 💼 Sourcing & Brand Takeaway: Smart factories hide this gate scar inside the lens groove or hinge pocket so the customer never sees or feels a rough spot on the frame.
59. Mold Shrinkage Rate
- 💡 In Plain English: How much plastic shrinks as it cools down from liquid hot to room temperature solid inside the steel mold.
📐 Technical Definition: The volumetric contraction percentage that an injection-molded polymer undergoes as it cools from molten liquid state to room-temperature solid inside the steel die.
- ⚙️ Factory Standards & Tolerances: TR90: 0.8% to 1.1%; Polycarbonate: 0.5% to 0.7%.
- 💼 Sourcing & Brand Takeaway: Factory engineers must calculate this exact shrinkage and make the steel mold slightly larger, or the finished frames will be too small and lenses won’t fit.
60. Thermal Annealing (Stress Baking)
- 💡 In Plain English: Baking molded plastic frames in warm ovens for two hours after injection to relax internal molecular tension, like a hot bath for the plastic.
📐 Technical Definition: A secondary manufacturing stage where molded TR90 or PC frames are soaked in hot air chambers to relieve molecular shear stresses induced during high-speed injection.
- ⚙️ Factory Standards & Tolerances: Heated at 110°C to 120°C for 120 minutes, followed by slow ambient furnace cooling.
- 💼 Sourcing & Brand Takeaway: Frames that skip annealing will crack and shatter as soon as an optician uses alcohol to clean them or snaps a tight prescription lens into the rim.
Cluster 7: Lens Optics, Geometry & Vacuum Coatings (Terms 61–68)
61. Base Curve (BC)
- 💡 In Plain English: The front curve of the lens and frame. A 2-Base is totally flat like modern high-fashion sunglasses; a 6-Base is traditional sunglasses; an 8-Base is wrapped around like sports cycling shields.
📐 Technical Definition: Base curve is the standardized measure of the front surface spherical curvature of an optical lens blank, calculated via the formula: BC = (n - 1) / r.
- ⚙️ Factory Standards & Tolerances: Industry benchmarks: 2-Base (flat fashion), 4-Base (modern optical), 6-Base (classic sunglass), 8-Base (full wrap sports). Tolerance: ±0.12D.
- 💼 Sourcing & Brand Takeaway: The frame and the lens MUST match base curves. Forcing a flat 2-Base lens into a curved 6-Base frame pops the eyewires wide open and ruins the shape.
62. CR-39 (Columbia Resin #39)
- 💡 In Plain English: The classic standard plastic for optical lenses. It is light, easy to tint into any custom sunglasses color, and provides crystal-clear vision with almost zero color distortion.
📐 Technical Definition: A thermoset polymer (allyl diglycol carbonate) invented in 1940, regarded as the global benchmark optical plastic due to its low weight, tintability, and crystal Abbe value (58).
- ⚙️ Factory Standards & Tolerances: Refractive index: 1.498; Abbe value: 58; specific gravity: 1.32.
- 💼 Sourcing & Brand Takeaway: Delivers the sharpest, clearest optical vision of any plastic lens. Compare lens types in our CR-39 vs. Nylon vs. Polycarbonate Guide.
63. TAC Polarized Lens
- 💡 In Plain English: Affordable polarized lenses made by sandwiching a microscopic glare-blocking filter film between thin layers of tri-acetate plastic.
📐 Technical Definition: A multi-layered laminated sunglass lens featuring a micro-thin polyvinyl alcohol (PVA) polarizing filter film sandwiched between protective cellulose triacetate layers.
- ⚙️ Factory Standards & Tolerances: Standard thicknesses: 0.74 mm, 1.0 mm, 1.1 mm; polarization efficiency: > 99%.
- 💼 Sourcing & Brand Takeaway: Blocks 99% of blinding road and water glare at an affordable cost. Great for lifestyle sunglasses, but not recommended for drill-mount rimless frames because it can delaminate if edges stay wet.
64. Optical Polyamide (Nylon Lens)
- 💡 In Plain English: The premium luxury lens material. Completely crack-proof, crystal clear, and can be drilled through without stress cracks forming around the holes.
📐 Technical Definition: A high-performance cast thermoplastic lens material offering exceptional optical clarity (Abbe 52), zero internal stress birefringence, and extreme crack resistance.
- ⚙️ Factory Standards & Tolerances: Refractive index: 1.530; Abbe value: 52; passes high-velocity missile impact tests.
- 💼 Sourcing & Brand Takeaway: The #1 choice for designer rimless sunglasses and luxury fashion brands that use drill-mount metal screws through the lenses.
65. Anti-Reflective Coating (AR / Anti-Glare)
- 💡 In Plain English: Microscopic invisible layers baked onto the lens inside a vacuum chamber that cancel out glare, reflections, and distracting ghost images.
📐 Technical Definition: A vacuum-deposited stack of alternating microscopic dielectric layers (metal oxides like SiO₂ and TiO₂) engineered to cancel surface reflections via destructive wave interference.
- ⚙️ Factory Standards & Tolerances: Multi-layer stack (5 to 16 layers) on high-vacuum PVD chambers; boosts luminous transmittance from 92% up to > 99.2%.
- 💼 Sourcing & Brand Takeaway: Essential on the BACK of sunglasses so wearers don’t see their own eyes reflected on the inside of the lens, and essential on optical lenses so people can see the wearer’s eyes clearly.
66. Hydrophobic & Oleophobic Topcoat (Lotus Effect)
- 💡 In Plain English: A nano-coating that makes the lens surface super slippery, like a lotus leaf. Water beads right off and skin oils or fingerprints wipe away with one gentle swipe.
📐 Technical Definition: A fluorocarbon nanocoating thermally baked as the outermost seal of an optical lens stack, creating an ultra-slick surface that repels water droplets, sweat, and fingerprints.
- ⚙️ Factory Standards & Tolerances: Water contact angle must exceed > 110°; tested for 10,000 cycle cheesecloth friction.
- 💼 Sourcing & Brand Takeaway: Customers hate dirty, smudged lenses. Having a hydrophobic topcoat makes sunglasses feel high-end every time the wearer cleans them.
67. Decentered Lens (Prism Neutralization)
- 💡 In Plain English: A curved sports lens whose optical center is specially shifted so you don’t get headaches or distorted vision when wearing curved sports sunglasses.
📐 Technical Definition: A lens engineered with asymmetric thickness distribution where the optical center is shifted relative to the geometric center to eliminate prism distortion in high-wrap frames.
- ⚙️ Factory Standards & Tolerances: Prismatic deviation held within < 0.12 prism diopters under spectrophotometer verification.
- 💼 Sourcing & Brand Takeaway: Mandatory for any sports sunglass with Base Curve 6, 7, or 8. If you use cheap flat lenses in a wrapped frame, wearers will experience eye fatigue and miss-judge distances while driving or cycling.
68. Abbe Value (Color Clarity Score)
- 💡 In Plain English: A score measuring how crisp and clear colors look through a lens without rainbow color fringing around objects. Higher numbers mean sharper, clearer vision.
📐 Technical Definition: A quantitative metric indicating the degree of chromatic aberration (color fringing) produced by an optical lens material as white light passes through it.
- ⚙️ Factory Standards & Tolerances: Higher is better: Glass (59) > CR-39 (58) > Nylon (52) > Polycarbonate (30).
- 💼 Sourcing & Brand Takeaway: Polycarbonate has a low Abbe value of 30, meaning people with strong prescriptions can see rainbow fringes around white text. CR-39 and Nylon provide crystal optical clarity.
Cluster 8: Ergonomics, Asian Fit & Bridge Anatomy (Terms 69–76)
69. Asian Fit (Low Bridge Fit / Alternative Fit)
- 💡 In Plain English: Frames specially sculpted for people with flatter nose bridges and higher cheekbones. The nose pads are taller, the bridge is narrower, and the tilt is flattened so the glasses never slide down your nose or rest on your cheeks when you smile.
📐 Technical Definition: An ergonomic frame geometry engineered for facial structures characterized by a flatter nasal crest, prominent cheekbones, and a wider craniofacial temple width.
- ⚙️ Factory Standards & Tolerances: Features extended nasal pads (+2.5 to +4.0 mm), narrower DBL (15–17 mm), flattened pantoscopic angle (5°–7°), and reduced wrap curve (< 4°).
- 💼 Sourcing & Brand Takeaway: Crucial for selling into Asian, Hispanic, or diverse global markets. Standard Western frames will slide right off low-bridge noses. Read our full comparison on Asian Fit vs. Western Fit Eyewear.
70. Western Fit (Standard European Fit)
- 💡 In Plain English: Traditional frame geometry designed for faces with high, prominent nose bridges and deep-set eyes.
📐 Technical Definition: Traditional optical frame geometry designed for craniofacial profiles featuring a higher, narrower nasal bridge with deep-set ocular orbits.
- ⚙️ Factory Standards & Tolerances: Standard DBL: 18 mm to 22 mm; pantoscopic tilt: 8° to 12°; standard shallow saddle pad heights.
- 💼 Sourcing & Brand Takeaway: The historical default for European and American brands. Selling standard Western acetate frames in Asian markets yields return rates above 30% unless modified with nose pad arms.
71. Built-In Acetate Saddle Pad (Molded Pad)
- 💡 In Plain English: Smooth nose pads carved directly out of the front acetate plastic. Clean, modern, and sleek with no metal arms to get bent or tangled in your hair.
📐 Technical Definition: Smooth, monolithic nasal support pads carved directly out of the primary acetate front stock during 5-axis CNC routing and finished via continuous barrel tumbling.
- ⚙️ Factory Standards & Tolerances: Pad projection height calibrated to 3.0 mm (Western) to 6.5 mm (Asian fit).
- 💼 Sourcing & Brand Takeaway: Sleek and minimalist, but cannot be adjusted once made. You must engineer the pad height correctly in your 3D CAD design before cutting acetate.
72. Goose-Neck Pad Arm
- 💡 In Plain English: The S-shaped metal wire brackets that hold soft silicone nose pads. Opticians can bend and adjust them in any direction with pliers for a tailored custom fit.
📐 Technical Definition: An S-curved or gooseneck adjustable metal wire bracket (brazed to metal rims or heat-staked into acetate) that holds modular snap-in or screw-in nose pads.
- ⚙️ Factory Standards & Tolerances: Fabricated from pure titanium or high-yield nickel silver; wire diameter: 0.9 mm to 1.2 mm.
- 💼 Sourcing & Brand Takeaway: The ultimate solution for universal fit. Allows a single frame model to comfortably fit any nose shape or bridge height worldwide.
73. Splay Angle
- 💡 In Plain English: The horizontal angle of the nose pads when viewed from above, matching how the sides of your nose widen out.
📐 Technical Definition: The horizontal angle formed between the flat face of the nose pad and the longitudinal sagittal plane of the wearer’s nose, viewed from directly above.
- ⚙️ Factory Standards & Tolerances: Anatomical benchmark is 25° to 30° outwards.
- 💼 Sourcing & Brand Takeaway: If the splay angle is wrong, only the front or back edge of the pad touches the nose, digging painful red marks into the skin.
74. Frontal Angle
- 💡 In Plain English: The vertical tilt of the nose pads when looking directly at the wearer’s face, matching how the bridge widens from top to bottom.
📐 Technical Definition: The vertical tilt angle formed between the vertical axis of the nose pad and the coronal facial plane when viewed directly from the front.
- ⚙️ Factory Standards & Tolerances: Standard target is 20° inward to mirror the natural downward widening taper of the human nasal bone.
- 💼 Sourcing & Brand Takeaway: Spreads the weight of the glasses evenly across the nose skin (ideal pressure target < 15 grams per square centimeter).
75. Temple Spread Angle (Open Temple Flare)
- 💡 In Plain English: The slight outward angle of the glasses arms when fully opened (typically 93° to 95°, slightly wider than a strict 90° right angle).
📐 Technical Definition: The outward lateral angle formed by the open temples relative to the frame front plane, measured at resting extension.
- ⚙️ Factory Standards & Tolerances: Nominal standard is 92° to 95° (allowing 2°–5° outward flare past 90°).
- 💼 Sourcing & Brand Takeaway: If arms open to exactly 90.0 degrees, they will painfully squeeze the sides of adult heads. 93° provides a comfortable, pressure-free fit right out of the box.
76. Mastoid Bend Curvature (Drop Bend)
- 💡 In Plain English: The ergonomic curve where the arm bends down behind the ear to keep the glasses from sliding forward off your face.
📐 Technical Definition: The downward anatomical curve molded into the terminal 30 mm to 40 mm tip of the temple stem to secure the frame behind the ear’s mastoid process.
- ⚙️ Factory Standards & Tolerances: Drop bend angle target: 40° to 45° downward, with a 5° to 8° inward tilt toward the skull base.
- 💼 Sourcing & Brand Takeaway: Must start exactly where the ear meets the head. If it bends too early, it lifts the glasses off the nose; if it bends too late, the glasses slide off when looking down at a phone.
Cluster 9: Branding, Laser & Decorative Crafts (Terms 77–83)
77. Fiber Laser Annealing (Black Laser Marking)
- 💡 In Plain English: Using high-tech laser pulses to heat titanium without burning it, turning the surface into crisp, permanent black logo lettering that will never rub off or fade.
📐 Technical Definition: A non-contact digital branding method using a focused 1064 nm fiber laser beam to either micro-ablate metal surfaces or thermally induce dark black oxidation marks (laser annealing) on titanium.
- ⚙️ Factory Standards & Tolerances: Beam focus spot: 0.02 mm; engraving depth: 0.03 mm to 0.1 mm.
- 💼 Sourcing & Brand Takeaway: Perfect for inner temple brand names, model numbers, and CE markings. Clean, surgical, and permanent. Discover more techniques in our Eyewear Logo Branding Guide.
78. Hot Foil Stamping
- 💡 In Plain English: Using a heated brass stamp to press real metallic gold or silver foil ribbons into the acetate plastic, leaving a luxurious debossed metallic logo.
📐 Technical Definition: A thermal transfer branding process where a heated metal brass die presses metallic or pigmented foil ribbons into raw acetate under pneumatic pressure.
- ⚙️ Factory Standards & Tolerances: Die temperature: 115°C to 135°C; impression depth: 0.1 mm to 0.15 mm; passes 3M 610 tape peel test.
- 💼 Sourcing & Brand Takeaway: The classic luxury method for gold logos on acetate. Low mold cost ($50–$80), making it ideal for brand startups launching with low 60-pair MOQs.
79. UP Metal Sticker (Electroformed 3D Badge)
- 💡 In Plain English: Ultra-thin 3D metal metallic stickers (in shiny gold, silver, or gunmetal) that are sunk flush into pre-carved pockets in the acetate temple arms.
📐 Technical Definition: Ultra-thin micro-electroformed pure nickel or copper logo emblems (available in 3D relief, brush-plated gold, or gunmetal) that mount into CNC-milled surface pockets.
- ⚙️ Factory Standards & Tolerances: Metal foil gauge: 0.06 mm to 0.12 mm; backed with industrial 3M 9448A high-tack adhesive.
- 💼 Sourcing & Brand Takeaway: Gives you the prestigious look of real cast metal jewelry emblems without the heavy weight or expensive casting mold fees.
80. Pad Printing (Tampography)
- 💡 In Plain English: Using a soft silicone stamp to print sharp, colorful ink logos onto curved glasses temples or demo lenses.
📐 Technical Definition: An indirect photogravure printing process where a silicone rubber pad picks up specialized two-component polyurethane inks from an etched steel cliché plate and transfers them onto curved surfaces.
- ⚙️ Factory Standards & Tolerances: Resolution capable of rendering 0.1 mm hair-thin lettering; cured via thermal convection ovens.
- 💼 Sourcing & Brand Takeaway: The most economical and versatile way to print crisp white model specifications and brand logos inside curvy temple arms.
81. Cloisonné Enamel Infill (Cold Vitreous Enamel)
- 💡 In Plain English: Filling tiny engraved metal logo cavities with liquid glossy enamel paint, cured under UV light into a glass-like jewel finish.
📐 Technical Definition: The artisanal bench application of liquid epoxy-enamel resins into precision-engraved metallic cavities on endpieces or temple tips, cured into a high-gloss glassy cabochon.
- ⚙️ Factory Standards & Tolerances: Resin dispensed via 0.25 mm micro-nozzle pneumatic needles; UV-cured under 365 nm lamps.
- 💼 Sourcing & Brand Takeaway: Adds jewelry-like color accents to frame corners, rivets, and temple tips. Very popular with luxury European fashion houses.
82. Diamond-Cut Edge Milling
- 💡 In Plain English: Using a genuine diamond knife spinning at 30,000 RPM to slice mirror-faceted edges into metal or acetate, shining like cut diamonds.
📐 Technical Definition: High-speed machining using monocrystalline natural diamond fly-cutter tools (up to 30,000 RPM) to slice mirror-reflective decorative facets into metal rims and temple edges.
- ⚙️ Factory Standards & Tolerances: Surface roughness Ra < 0.01 µm directly off the diamond tool with zero secondary polishing.
- 💼 Sourcing & Brand Takeaway: Creates dazzling, sparkling reflections on titanium bridges and temple edges without needing chrome plating.
83. Double-Shot Injection Co-Molding
- 💡 In Plain English: Molding two different plastics in the same machine at the same time: a rigid plastic frame fused together with soft non-slip rubber on the nose and ear pads.
📐 Technical Definition: A sophisticated two-stage molding process where a rigid plastic core (e.g., TR90) is over-molded inside the same machine with a soft elastomer (e.g., Megol or TPU rubber).
- ⚙️ Factory Standards & Tolerances: Mold alignment registration held to ±0.02 mm; molecular peel adhesion > 4.0 N/mm.
- 💼 Sourcing & Brand Takeaway: Eliminates messy glue. Yields seamless non-slip rubber nose bridges and ear grips on high-performance sports and tactical sunglasses.
Cluster 10: Testing, Compliance & Quality Standards (Terms 84–110)
84. ISO 12870 (Global Spectacle Frames Standard)
- 💡 In Plain English: The international lawbook for eyeglass frames. It defines mandatory safety, durability, sweat resistance, and flammability tests that every frame must pass to be legally sold in stores.
📐 Technical Definition: The internationally recognized harmonized standard establishing mandatory performance, mechanical endurance, dimensional tolerances, and biocompatibility requirements for spectacle frames.
- ⚙️ Factory Standards & Tolerances: Outlines rigorous testing protocols for sweat corrosion, bridge deformation, optical radiation exposure, and flammability resistance.
- 💼 Sourcing & Brand Takeaway: Mandatory baseline for selling frames in Europe, North America, and Australia. Certified ISO 12870 compliance eliminates customs seizure headaches.
85. CE Marking & EU 2016/425 (European Safety Certification)
- 💡 In Plain English: The CE mark printed on the inside arm of sunglasses certifying that they block harmful UV light and comply with European personal protective equipment laws.
📐 Technical Definition: The official conformity certification marking affixed to all sunglasses imported into the European Economic Area, verifying compliance with EU 2016/425 PPE Annex II essential health directives.
- ⚙️ Factory Standards & Tolerances: Requires technical file dossier (Technical Construction File), Declaration of Conformity (DoC), and EN ISO 12312-1 certification.
- 💼 Sourcing & Brand Takeaway: Non-negotiable for selling sunglasses anywhere in Europe. Shipments without valid CE certificates face immediate quarantine and destruction at European customs.
86. FDA 21 CFR 801.410 (Drop Ball Impact Test)
- 💡 In Plain English: The US legal requirement where a heavy steel ball is dropped from 50 inches (1.27 m) directly onto the lens. The lens must not shatter or chip.
📐 Technical Definition: The United States Federal regulation mandating that all commercial sunglass and prescription lenses pass an impact test with a 5/8-inch (16 mm) steel ball dropped from a height of 50 inches.
- ⚙️ Factory Standards & Tolerances: Steel ball weight: approx. 16 grams; lens must not fracture, crack, or flake upon impact.
- 💼 Sourcing & Brand Takeaway: Every single box of sunglasses entering US customs MUST have an accompanying Drop Ball Test Certificate from an FDA-registered manufacturer like Hermitin.
87. EN 16128 (Nickel Release Sweat Test)
- 💡 In Plain English: A strict European chemical test checking how much nickel leaks out of metal glasses when exposed to human sweat, protecting wearers from itchy skin allergies.
📐 Technical Definition: The European reference test method simulating human dermal sweat contact to measure the quantity of nickel ions leaching from metal components contacting the wearer’s skin.
- ⚙️ Factory Standards & Tolerances: Maximum legal nickel release threshold is < 0.5 µg/cm²/week (and < 0.28 µg/cm²/week for post assemblies).
- 💼 Sourcing & Brand Takeaway: Crucial for metal frames using Monel or nickel alloys. Requires dense gold, titanium, or IP barrier plating plus baked clear sealants to pass.
88. Hinge Endurance Fatigue Rig (50,000 Cycle Machine)
- 💡 In Plain English: A robotic machine that grabs the glasses arms and forcefully opens and closes them 20,000 to 50,000 times non-stop to verify that the hinges never snap or get loose.
📐 Technical Definition: An automated pneumatic laboratory testing machine that repeatedly opens and closes frame temples from 0° through 95° at a regulated frequency (30 to 40 cycles/minute).
- ⚙️ Factory Standards & Tolerances: Standard test run: 20,000 cycles for basic frames; 50,000 cycles for premium OBE/spring hinges.
- 💼 Sourcing & Brand Takeaway: Frames must maintain smooth friction after 20,000 cycles without screws falling out or knuckles cracking.
89. Bridge Deformation & Strength Rig
- 💡 In Plain English: A machine that anchors the rims and pushes hard down on the nose bridge with 40 Newtons of force to prove the bridge won’t bend or snap in half.
📐 Technical Definition: An ISO 12870 mechanical testing apparatus that applies a cycling vertical displacement load (5 mm deflection at 40 N force) to the nasal bridge while rims are anchored.
- ⚙️ Factory Standards & Tolerances: Permanent post-test bridge deformation must be < 1.5% of initial distance between centers; zero weld detachment.
- 💼 Sourcing & Brand Takeaway: Guarantees that when a customer sits on their glasses or stuffs them into a backpack, the bridge won’t snap in half.
90. Spectrophotometer UV400 Verification
- 💡 In Plain English: A high-tech laboratory laser machine that scans lenses with light to prove beyond doubt that they block 100% of dangerous UV-A and UV-B radiation up to 400 nanometers.
📐 Technical Definition: High-precision laboratory spectroscopy measuring the percentage of ultraviolet radiation transmitted through a lens across the spectrum from 280 nm to 400 nm.
- ⚙️ Factory Standards & Tolerances: UV400 standard mandates < 0.5% transmittance between 280 nm and 380 nm, and < 1.0% transmittance up to 400 nm.
- 💼 Sourcing & Brand Takeaway: The scientific proof behind the ‘100% UV Protection’ sticker on your sunglasses. Every production batch at Hermitin receives spectrophotometer verification.
91. Salt Spray & Artificial Sweat Corrosion Chamber (ASTM B117)
- 💡 In Plain English: Blowing hot, salty mist and acidic artificial sweat all over frames for 4 days inside a sealed glass chamber to prove they will never rust or tarnish at the beach.
📐 Technical Definition: An accelerated environmental stress test where metal and plated frames are exposed to atomized 5% sodium chloride saline fog at 35°C, or immersed in synthetic acidic sweat baths.
- ⚙️ Factory Standards & Tolerances: Test duration: 24 to 96 hours continuous salt spray; examined for green verdigris corrosion, plating peel, or pitting.
- 💼 Sourcing & Brand Takeaway: Proves whether gold, silver, or IP plating will survive 2+ years of beach vacations, sunscreen, and sweaty workouts without flaking.
92. Go / No-Go Caliper Inspection Gauge
- 💡 In Plain English: Precision hardened-steel metal templates that factory inspectors use on the assembly line: if the frame fits inside the ‘Go’ slot and stops at the ‘No-Go’ slot, its size is 100% perfect.
📐 Technical Definition: Precision CNC-hardened tool steel templates used by cleanroom quality inspectors to instantaneously verify whether frame dimensions fall within acceptable upper/lower tolerance envelopes.
- ⚙️ Factory Standards & Tolerances: Gauge ground to ±0.005 mm accuracy.
- 💼 Sourcing & Brand Takeaway: Eliminates human error on high-speed assembly lines, guaranteeing every customer receives the exact size specified in your CAD tech pack.
93. Cross-Hatch Adhesion Test (Tape Peel Test)
- 💡 In Plain English: Scratching a grid of tiny knife cuts into painted or printed logos, slapping industrial 3M tape over it, and violently ripping it off. Zero paint or logo flakes may come off.
📐 Technical Definition: A destructive surface coating test where a lattice grid of micro-incisions (1 mm spacing) is scored into a painted or plated surface, followed by rapid peeling with 3M pressure-sensitive tape.
- ⚙️ Factory Standards & Tolerances: Requirement: Class 0 (flawless adhesion with 0% coating flaking along grid intersections under ISO 2409).
- 💼 Sourcing & Brand Takeaway: Validates that rubberized soft-touch paints and printed brand logos will never peel or flake off during daily use.
94. Polariscope Strain Analyzer
- 💡 In Plain English: A device with polarized light filters that lets inspectors ‘see’ hidden stress inside glasses lenses, showing rainbow halos if a lens was cut too tight and pinched by the frame.
📐 Technical Definition: An optical inspection instrument utilizing two crossed polarizing filters to visualize internal molecular strain patterns (photoelastic birefringence) inside edged lenses.
- ⚙️ Factory Standards & Tolerances: Color fringes must show balanced, gentle rainbow halos with zero sharp, concentrated white ‘pinch-point’ nodes.
- 💼 Sourcing & Brand Takeaway: Catches oversized lenses before they cause headaches, lens warpage, or chipped glass edges.
95. Tech Pack (Technical Specification Package)
- 💡 In Plain English: The complete master blueprint for your glasses. It includes 2D dimensioned CAD drawings, 3D STEP files, pantone color codes, hinge choices, and packaging artwork.
📐 Technical Definition: The complete engineering document package provided by an eyewear brand or developed by Hermitin’s engineers. Includes 2D dimensioned CAD drawings, 3D STEP surface files, pantoscopic angles, pantone color codes, hinge specs, and acceptance quality limits (AQL).
- ⚙️ Factory Standards & Tolerances: Dimensioned to ±0.05 mm engineering tolerances.
- 💼 Sourcing & Brand Takeaway: A detailed tech pack eliminates miscommunication. If you only have a rough sketch, Hermitin’s engineering team can turn it into a production-ready CAD tech pack.
96. DFM Review (Design for Manufacturability)
- 💡 In Plain English: The expert factory audit where tooling engineers review your 3D design to catch flaws (like walls that are too thin to inject or corners too sharp to polish) before cutting expensive steel molds.
📐 Technical Definition: The preliminary engineering audit conducted by factory toolers before cutting steel molds or ordering acetate slabs, optimizing designs for high-yield production.
- ⚙️ Factory Standards & Tolerances: Evaluates draft angles, wall thickness uniformity, stress concentration points, and tooling clearances.
- 💼 Sourcing & Brand Takeaway: Saves thousands of dollars and months of lost time by catching manufacturing impossibilities while they are still digital CAD files.
97. Rapid Prototyping (RP 1:1 Sample)
- 💡 In Plain English: Machining a real physical prototype frame out of a solid block of acetate in our workshop so you can hold it, try it on your face, and check the fit before paying for mass production.
📐 Technical Definition: A functional pre-production physical prototype machined directly from solid acetate on 5-axis CNCs or high-resolution SLA/SLS 3D printers.
- ⚙️ Factory Standards & Tolerances: Dimensional accuracy held to ±0.1 mm of the approved 3D CAD model.
- 💼 Sourcing & Brand Takeaway: Never start mass production without an RP sample! Explore our 1:1 Custom Eyewear Prototyping Services to see real workshop builds.
98. Tolerance Stack-Up
- 💡 In Plain English: When tiny 0.1 mm variations in the front lug, hinge ring, and screw hole add up together, causing one arm to open crooked or sit higher than the other.
📐 Technical Definition: The cumulative effect of individual manufacturing variations across multiple assembled parts (e.g., front lug tolerance + hinge barrel play + screw thread looseness).
- ⚙️ Factory Standards & Tolerances: Total assembly stack-up must be controlled within ±0.3 mm of absolute horizontal alignment.
- 💼 Sourcing & Brand Takeaway: Cheap factories ignore stack-up, resulting in wobbly frames that sit crooked on your face. Hermitin engineers tight tolerances at every component interface.
99. Draft Angle
- 💡 In Plain English: The slight inward slope (like a paper cup) designed into plastic molds so the finished glasses frame slides out smoothly without sticking or getting scratched.
📐 Technical Definition: The slight inward taper (typically 0.5° to 1.5°) engineered into the vertical walls of injection mold cavities to allow molded frames to eject cleanly without drag marks.
- ⚙️ Factory Standards & Tolerances: Standard draft angle target: 1.0° to 1.5° on all vertical core surfaces.
- 💼 Sourcing & Brand Takeaway: Essential for injection molding. If draft angles are missing, the frame gets stuck inside the steel mold and scratches on every cycle.
100. Sink Mark Flaw
- 💡 In Plain English: An ugly dent or depression on the surface of plastic glasses caused when thick sections of plastic cool unevenly and shrink inward.
📐 Technical Definition: A surface depression flaw in injection-molded frames occurring over thick sections caused by uneven cooling contraction where the inner core shrinks away from the outer shell.
- ⚙️ Factory Standards & Tolerances: Maximum allowable sink depth on non-cosmetic surfaces is < 0.05 mm; zero sink marks permitted on front eyewires.
- 💼 Sourcing & Brand Takeaway: Fixed during DFM by coring out the back of thick lugs or optimizing injection pack pressure.
101. Anodizing (Electrolytic Color Oxidation)
- 💡 In Plain English: An electrochemical bath that transforms raw aluminum and titanium into brilliant, scratch-resistant colors that are physically part of the metal, not painted on.
📐 Technical Definition: An electrochemical process used primarily on aluminum and titanium eyewear to grow a protective, colored oxide layer that is integrated into the metal rather than plated on top.
- ⚙️ Factory Standards & Tolerances: Oxide layer thickness: 10 µm to 25 µm; surface hardness exceeds HV 400.
- 💼 Sourcing & Brand Takeaway: Will never peel, chip, or flake because the color is grown directly from the titanium itself.
102. Ceramic Cermet Nose Pads
- 💡 In Plain English: Luxury high-tech nose pads made of solid white or black ceramic. They never yellow, never get sticky, and feel silky smooth on the skin.
📐 Technical Definition: Sintered high-tech zirconium ceramic nose pads offering absolute chemical inertness, silky skin glide, and immunity to cosmetic discoloration.
- ⚙️ Factory Standards & Tolerances: Vickers hardness > HV 1,200; 100% hypoallergenic.
- 💼 Sourcing & Brand Takeaway: The ultimate upgrade for luxury sunglasses. Unlike cheap clear silicone pads that turn yellow after 3 months, ceramic pads stay pristine forever.
103. Spring Core Wire (Flex Core)
- 💡 In Plain English: A temple core wire that has a micro-spring hinge welded directly to the wire stem, making temple arms slimmer and cleaner.
📐 Technical Definition: A specialized temple core wire containing an integrated micro-spring hinge welded directly to the wire stem, simplifying assembly and slimming down external temple silhouettes.
- ⚙️ Factory Standards & Tolerances: Integrated spring stroke: 2.0 mm to 3.0 mm; fatigue cycle tested to > 30,000 openings.
- 💼 Sourcing & Brand Takeaway: Allows designers to create ultra-sleek, slim acetate temples that still flex comfortably outward.
104. Water Transfer Printing (Hydro-Dipping)
- 💡 In Plain English: Floating a decorative ink film (like camouflage, carbon fiber, or wood grain) on water, then dipping the glasses into it to wrap the pattern seamlessly around 3D curves.
📐 Technical Definition: A decorative printing craft where a water-soluble film floating on a water bath transfers complex patterns seamlessly around 3D curved frame contours.
- ⚙️ Factory Standards & Tolerances: Sealed with automotive-grade 2K polyurethane UV clear coat.
- 💼 Sourcing & Brand Takeaway: Enables intricate camouflage, marble, and wood textures on lightweight TR90 sports frames.
105. Hydro-Forming
- 💡 In Plain English: Using high-pressure hydraulic water inside a steel mold to blow metal tubes into smooth, organic curved shapes without any ugly welds.
📐 Technical Definition: Shaping ultra-thin metal tubes or sheet eye wires using pressurized hydraulic fluid inside a closed die, producing organic tubular frame bridges without weld seams.
- ⚙️ Factory Standards & Tolerances: Hydraulic pressure: up to 1,500 bar; wall thickness consistency within ±0.03 mm.
- 💼 Sourcing & Brand Takeaway: Enables ultra-futuristic, aerodynamic tubular bridge designs that are impossible with standard stamping tools.
106. Wire Core Guilloché Chasing
- 💡 In Plain English: Engraving intricate diamond-cut geometric patterns along the metal wire core, glowing beautifully through crystal clear acetate arms.
📐 Technical Definition: Intricate geometric engine-turned patterns engraved along the visible length of a wire core, illuminated through crystal translucent acetate temples.
- ⚙️ Factory Standards & Tolerances: Engraving line resolution: 0.05 mm; polished to high specular reflectivity.
- 💼 Sourcing & Brand Takeaway: A signature visual hallmark of luxury heritage eyewear (such as Jacques Marie Mage or Oliver Peoples).
107. Pinhole Occluder Diagnostic
- 💡 In Plain English: A clinical optical tool with tiny pinholes used to verify whether a customer’s blurred vision is caused by the frame fitting too close or an incorrect lens prescription.
📐 Technical Definition: An optical inspection diagnostic tool with micro-perforations used during clinical fitting to verify whether visual degradation stems from frame vertex distance or refractive power errors.
- ⚙️ Factory Standards & Tolerances: Hole diameter: 1.2 mm optical pinholes.
- 💼 Sourcing & Brand Takeaway: Helps opticians diagnose whether fitting errors (like improper pantoscopic tilt or vertex distance) are ruining the wearer’s vision.
108. Photochromic Half-Life (Transition Activation)
- 💡 In Plain English: How fast transition lenses turn dark when you walk into the sun, and how fast they clear up when you step back indoors.
📐 Technical Definition: The precise time in seconds required for a light-adaptive transition lens to darken to 50% opacity upon direct UV exposure, or fade back to clear indoors.
- ⚙️ Factory Standards & Tolerances: Industry benchmark: Darkens to 70% in < 30 seconds; fades back to clear in < 60 seconds at 23°C.
- 💼 Sourcing & Brand Takeaway: Quality photochromic lenses react fast in all temperatures, while cheap transition lenses stay sluggish in the winter.
109. Lens Groover & Edger Calibration
- 💡 In Plain English: Calibrating computerized optical lens edgers so the bevel around the edge of the lens fits into the frame groove like a hand in a glove.
📐 Technical Definition: The calibration standard ensuring that CNC optical edgers bevel optical lenses to match the exact curvature and depth of the frame’s internal V-bevel groove.
- ⚙️ Factory Standards & Tolerances: Bevel angle calibration held to 115° ±2°; bevel apex position held to ±0.03 mm.
- 💼 Sourcing & Brand Takeaway: Guarantees that lenses snap in with a satisfying click and stay firmly locked without rattling.
110. AQL Sampling Standard (Acceptable Quality Limit)
- 💡 In Plain English: The international mathematical quality control standard used to inspect your eyewear order before it is packed into shipping cartons.
📐 Technical Definition: The mathematical sampling standard (ISO 2859-1 / ANSI/ASQ Z1.4) utilized during pre-shipment inspections to determine batch acceptance based on statistical sampling.
- ⚙️ Factory Standards & Tolerances: Hermitin operates under strict AQL 1.0 Major / AQL 2.5 Minor benchmarks for all export shipments.
- 💼 Sourcing & Brand Takeaway: Protects your brand. Major defects (like scratched lenses or broken hinges) have a virtually zero-tolerance threshold of 1.0, ensuring your retail boxes arrive flawless.
How to Turn These Specifications into Commercial Success
Understanding optical engineering terminology does more than prevent factory mistakes—it transforms how you build and scale an eyewear brand:
- Faster Sample Iterations: When your tech packs specify exact tolerances, materials, and hardware systems up front, pre-production prototypes land right on the first revision, reducing sample lead times from 90 days down to 21 days.
- Transparent, Predictable Costing: Knowing the difference between 3-barrel vs. 5-barrel hinges, or cold runner vs. hot runner molds, lets you negotiate factory quotations with confidence, eliminating hidden upcharges or vague “quality tiers.”
- Retail Return Rates Under 0.5%: Sizing your bridge angles, panto tilt, and acetate aging protocols correctly protects your brand’s reputation against consumer returns, squeaky hinges, and warped frames.
Partner with Hermitin Optical: Engineering-First Eyewear Manufacturing
At Hermitin Optical, our dual-factory infrastructure bridges high-precision optical lens casting in Danyang with scalable cellulose acetate and titanium frame manufacturing in Taizhou. Whether you are launching a boutique private label collection with flexible 60-pair MOQs or scaling custom-tooled designs across global distribution, our English-speaking engineering team reviews your CAD files for complete Design for Manufacturability (DFM).
- 📐 Have a 2D sketch or 3D CAD design? Explore Our Prototyping & Custom Sample Cases to see real workshop builds.
- ⚡ Need instant production budgeting? Use our interactive Eyewear Instant Quote Calculator to model landed costs.
- 📦 Looking for in-stock, private-label ready models? Download Our Complete Eyewear Catalogs & NDA Templates.